
GoPro Remote Holder - For timelapse
Obliczymy ostateczną cenę na podstawie wybranego pliku. Sprawdzisz ją i zaakceptujesz przed płatnością.
Wstępna wycena dla PETG
0,55 € – 0,67 € netto (bez VAT)
Dla pliku: Extruder Clip_0.2mm_PETG_MK3S_39m.gcode
To wstępna wycena jednego pliku. Dokładną cenę poznasz przed zamówieniem.
Plik i założenia wyceny
Plik użyty do wyceny
Średnia wycena orientacyjna: 0,61 € netto (środek widełek).
- Masa podana przez autora
- 7 g
- Czas druku podany przez autora
- 39,6 min
- Materiał u źródła
- PET
- Materiał wyceny
- PETG
- Drukarka wyceny
- Bambu Lab P1S - 0.4 nozzle
- Proces wyceny
- 0.20mm Standard
Orientacyjna wycena wyłącznie wybranego pliku, oparta na masie i czasie druku podanych przez autora. Warianty plików nie są sumowane. Ostateczna cena zostanie obliczona po analizie pliku.
Zapisane na tym urządzeniu.
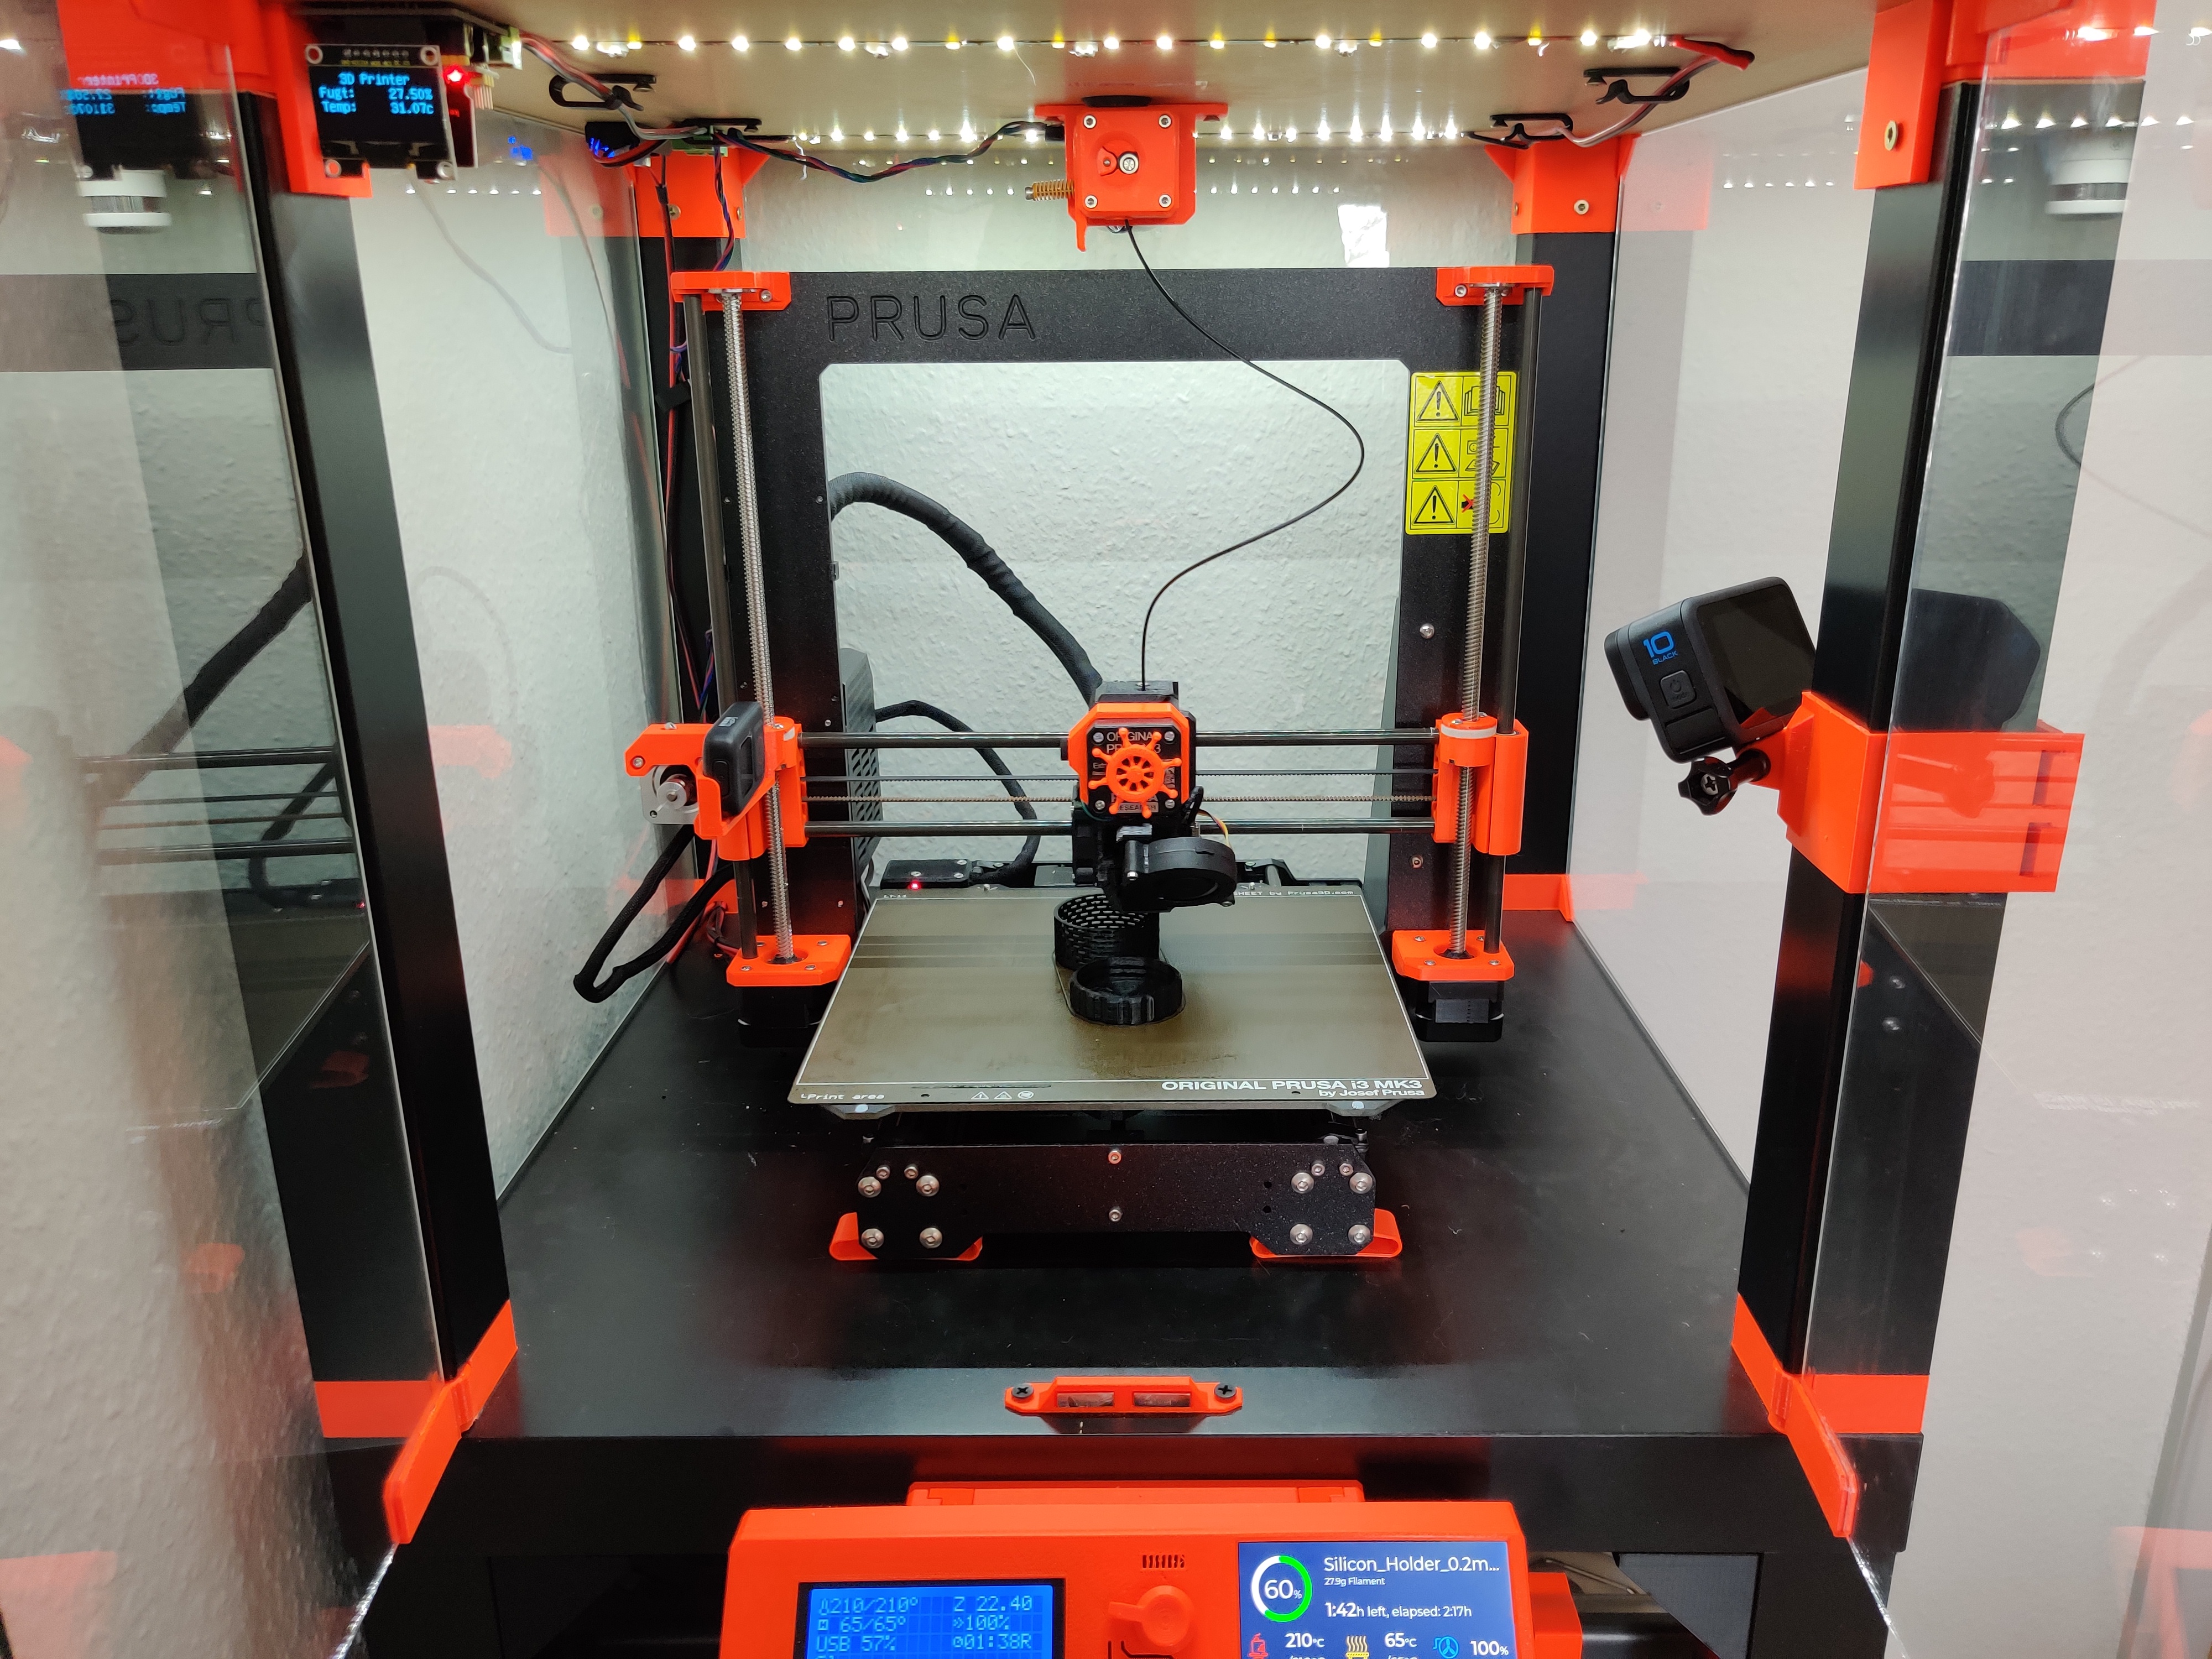
Simple design for holding a GoPro Remote, to be use for timelapse.
- Ocena
- 5 / 5
- Polubienia
- 3
- Pobrania
- 41
- Wydruki
- 1
- Wyświetlenia
- 588
- Oceny
- 1
Aktualizacja u źródła:
Informacje o modelu
- Źródło
- Printables
- Kategoria
- Other Printer Parts & Upgrades
- Licencja
- Creative Commons — Attribution — Noncommercial
I like the idea from EddiePrints, but wanted a version where the Remote was not zip tied on, so i easy could remove it and use it somewhere else.
Also wanted it on the other side of the printer. By this, you have to remove the remote on start op when the printer is running it's Z level, and add the remote when the printer purge its nozzle.

I also made a Extruder Snap on, so it could trigger the remote. Just add a felt pad on the side.
Add those Custom G-Code to your slicer so the printer will trigger the GoPro Remote on layer change
After layer change G-Code
;AFTER_LAYER_CHANGE
G1 X1 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G1 X6 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G4 P1250 ;Wait for 1250ms
;[layer_z]
If you like a picture after last layer, add this in “End G-Code”
G1 X1 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G1 X6 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G4 P1250 ;Wait for 1250ms
G1 X6 Y200 F{travel_speed*60} ;Move away from the print