
GoPro Remote Holder - For timelapse
We calculate the final price from your selected file. You review and accept it before payment.
Preliminary estimate for PETG
€0.55 – €0.67 net (excluding VAT)
For file: Extruder Clip_0.2mm_PETG_MK3S_39m.gcode
This is an estimate for one file. You’ll confirm the exact price before ordering.
File and estimate settings
File used for this estimate
Average indicative estimate: €0.61 excluding VAT (range midpoint).
- Weight reported by the author
- 7 g
- Print time reported by the author
- 39.6 min
- Source material
- PET
- Estimate material
- PETG
- Estimate printer
- Bambu Lab P1S - 0.4 nozzle
- Estimate process
- 0.20mm Standard
Indicative estimate for the selected file only, based on the author’s weight and print time. File variants are not added together. The final price is calculated after file analysis.
Saved on this device.
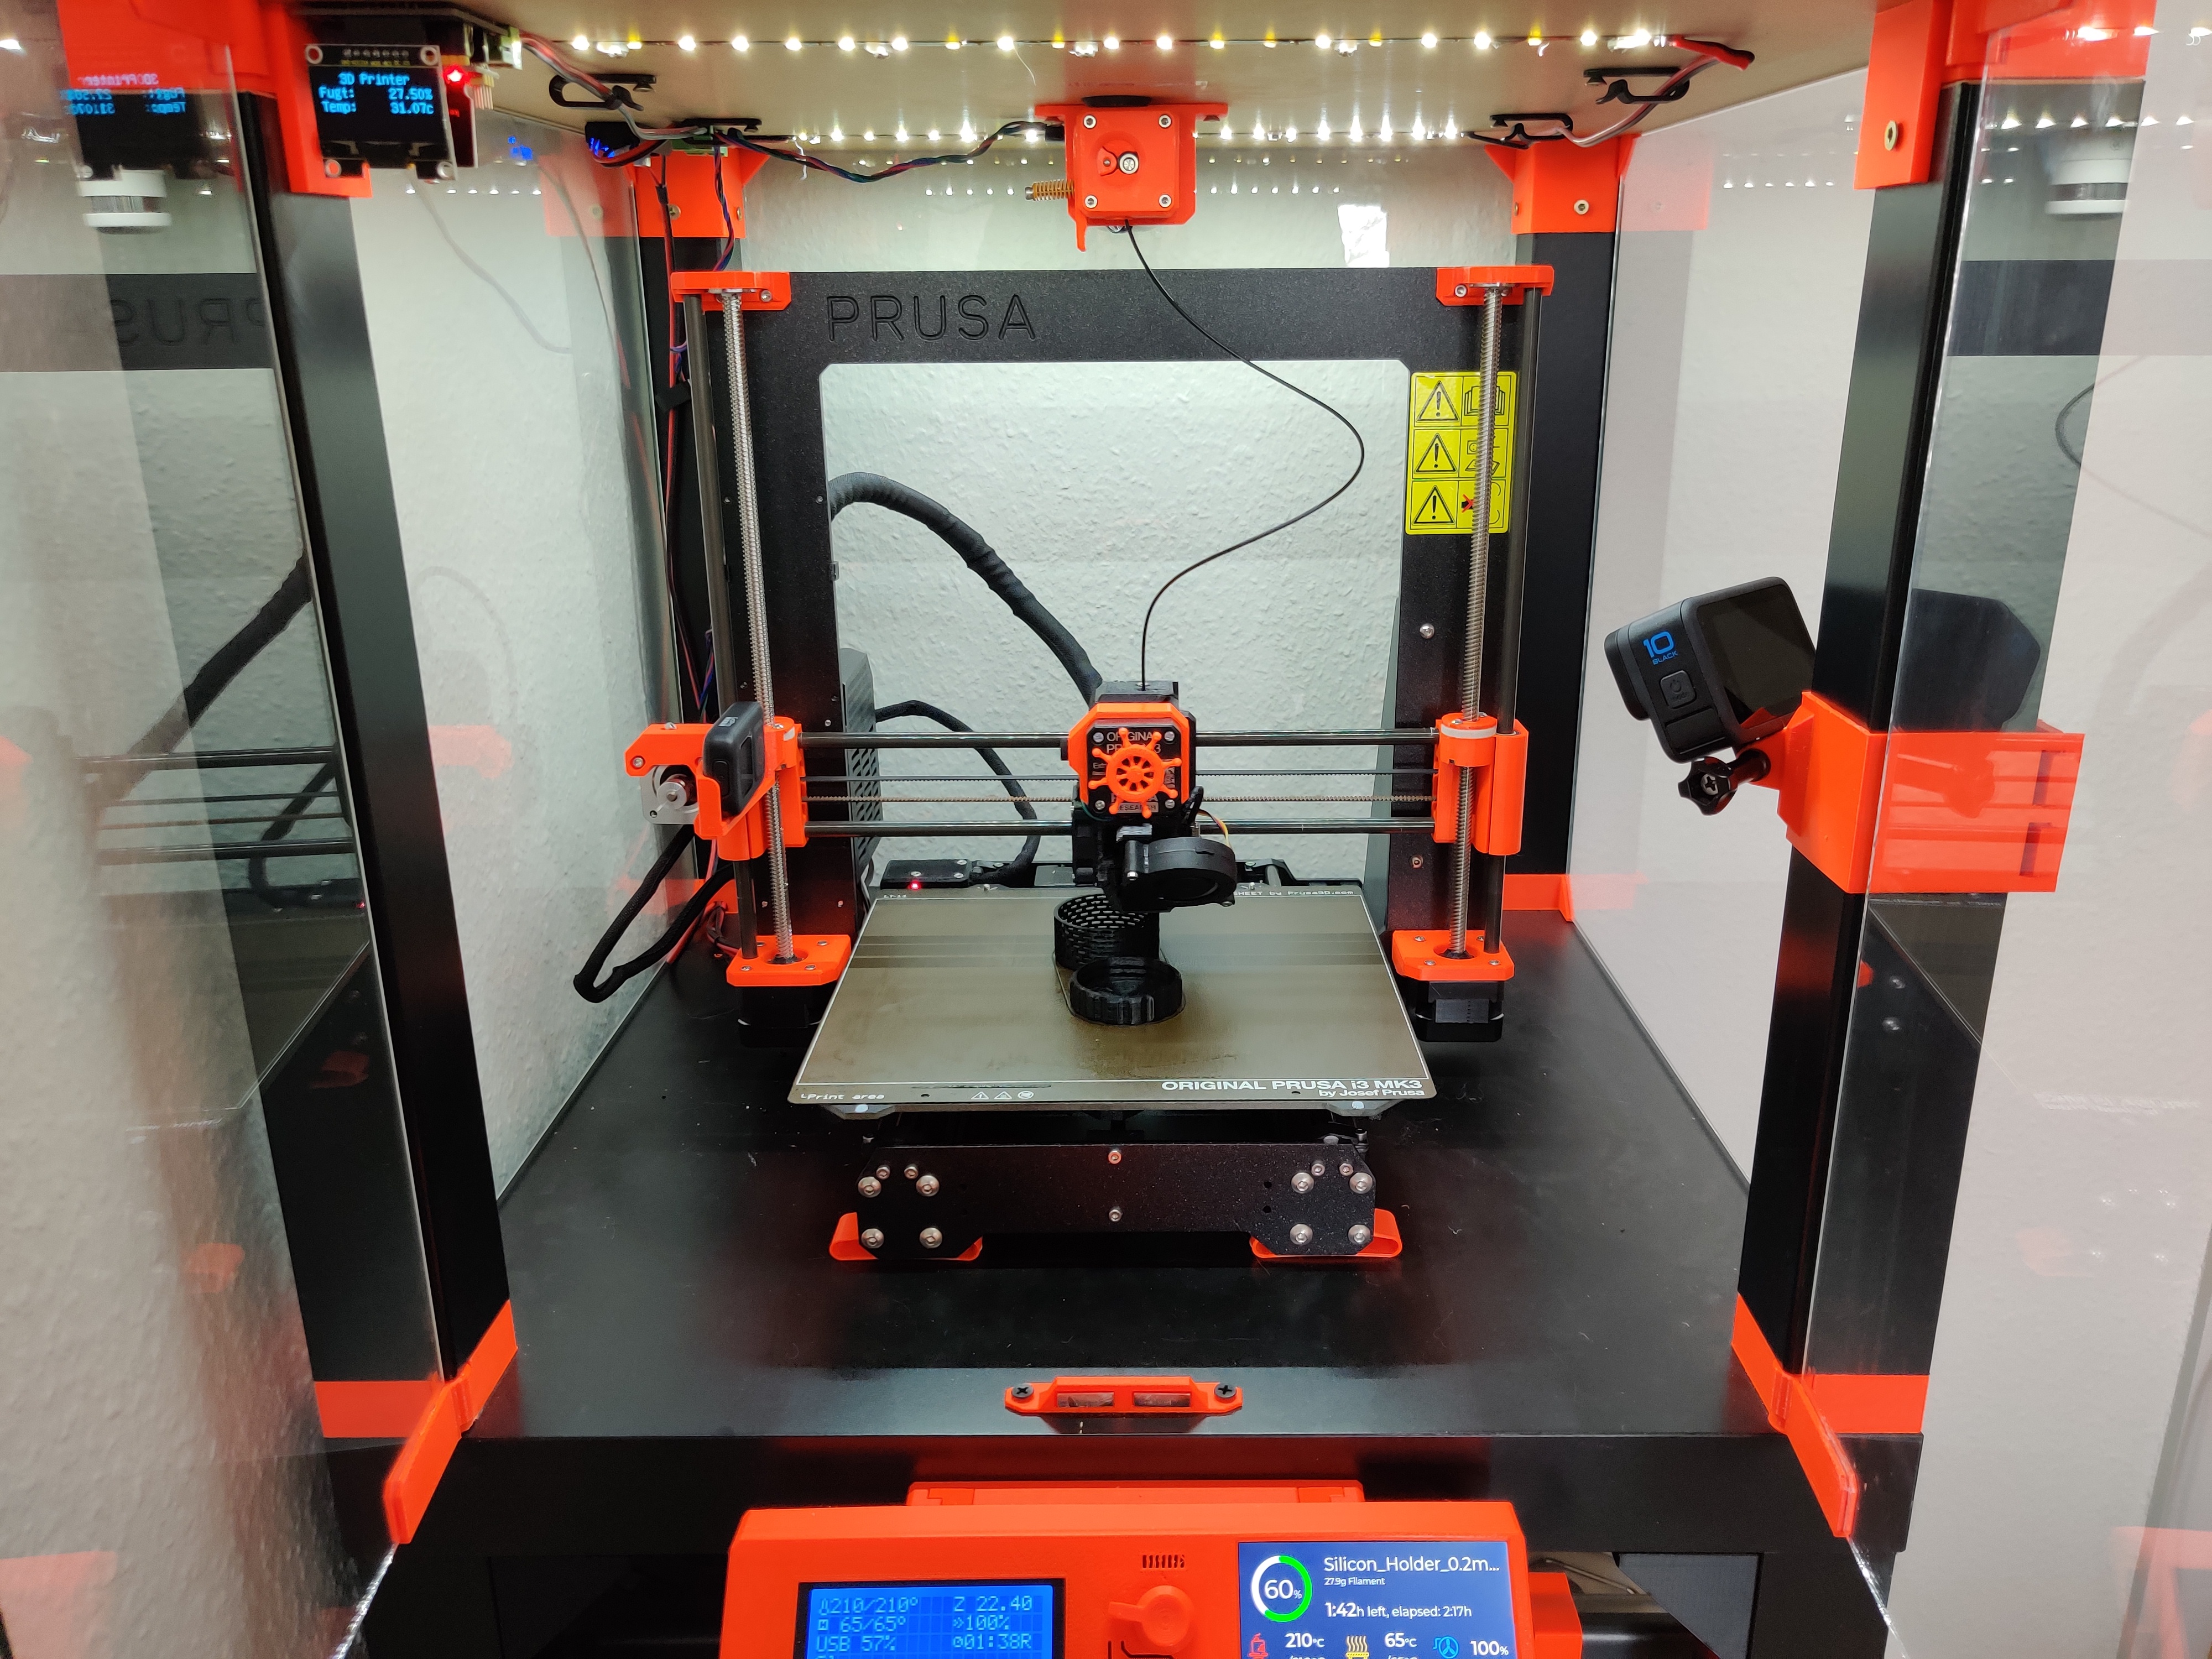
Simple design for holding a GoPro Remote, to be use for timelapse.
- Rating
- 5 / 5
- Likes
- 3
- Downloads
- 41
- Makes
- 1
- Views
- 588
- Reviews
- 1
Updated at source:
Model information
- Source
- Printables
- Category
- Other Printer Parts & Upgrades
- License
- Creative Commons — Attribution — Noncommercial
I like the idea from EddiePrints, but wanted a version where the Remote was not zip tied on, so i easy could remove it and use it somewhere else.
Also wanted it on the other side of the printer. By this, you have to remove the remote on start op when the printer is running it's Z level, and add the remote when the printer purge its nozzle.

I also made a Extruder Snap on, so it could trigger the remote. Just add a felt pad on the side.
Add those Custom G-Code to your slicer so the printer will trigger the GoPro Remote on layer change
After layer change G-Code
;AFTER_LAYER_CHANGE
G1 X1 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G1 X6 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G4 P1250 ;Wait for 1250ms
;[layer_z]
If you like a picture after last layer, add this in “End G-Code”
G1 X1 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G1 X6 Y125 F{travel_speed*60} ;Move away from the print
G4 S0 ;Wait for move to finish
G4 P1250 ;Wait for 1250ms
G1 X6 Y200 F{travel_speed*60} ;Move away from the print